Modular split construction for confined tunnel spaces, over 30% faster coordination of development and transport work, 4+2 hydraulic valve, dedicated hydraulic lock on every actuator cylinder.
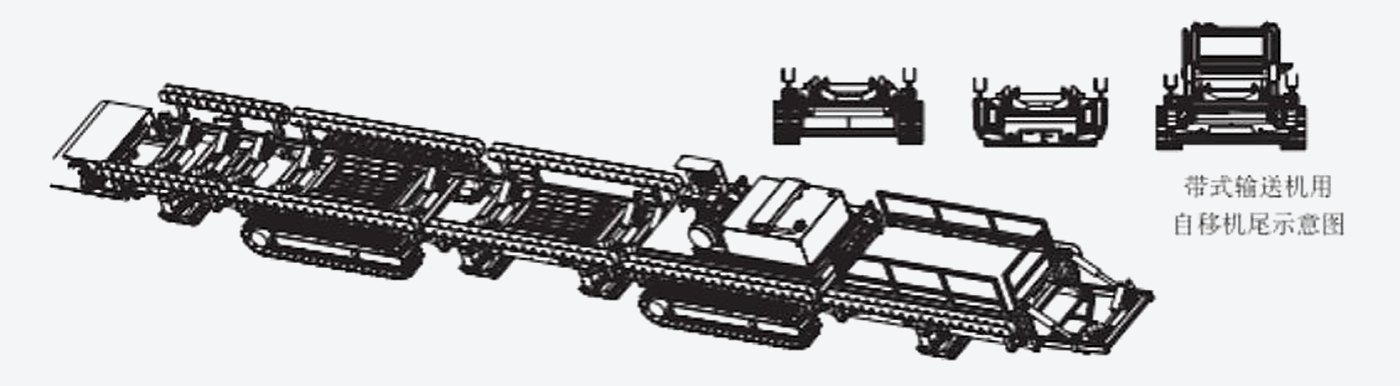
The Martel self-advancing tail uses a modular split architecture: the frame, self-moving carriage and advance mechanism can be disassembled and assembled separately. This simplifies underground transport and installation — especially where the tunnel entry space is limited.
Symmetric travel rails on both sides, together with the self-moving carriage and several sets of support cylinders plus a push cylinder, produce a smooth stepping motion of the frame. Without frequent dismantling of the anchored holding system, the tail works in synchronisation with the roadheader second conveyor.

The modular construction and the elimination of frequent anchor dismantling cut the auxiliary time spent moving equipment.
The "over 30%" figure is as stated by the manufacturer. Actual improvement depends on site conditions, cycle time and work organisation.
High-pressure emulsion, 4+2 six-way valve and a dedicated hydraulic lock on every cylinder.
The working medium is high-pressure emulsion from the working face — the standard source available at a coal mine.
The six-section valve controls the carriage, the travel rails and the slide blocks.
Every actuator cylinder has a dedicated hydraulic lock — reliable hold in any position.
On sudden loss of supply or a pressure surge the frame cannot shift by itself.
As stated by the manufacturer. Our engineer confirms the exact figures for your configuration after receiving the project data.
Download Specifications (PDF)| Product type | Martel self-advancing tail section |
|---|---|
| Construction | Modular split design — frame, self-moving carriage and advance mechanism assemble separately |
| Area of use | Work in confined tunnel (roadheader) entries |
| Advance drive | Symmetric travel rails on both sides plus self-moving carriage |
| Power elements | Several sets of support cylinders and a push cylinder working together for a smooth frame step |
| Step motion | Walking self-advance without frequent dismantling of the anchored holding system |
| Hydraulic medium | High-pressure emulsion from the working face |
| Hydraulic valve | 4+2 six-way valve |
| Control stations | One at the head end and one at the tail end — operator position is selectable |
| Hydraulic locks | Dedicated hydraulic lock on every actuator cylinder — reliable hold in any position |
| Fail-safe | On sudden loss of supply or pressure fluctuation the frame cannot move by itself under its own weight or external forces |
| Hydraulic lines | Abrasion-resistant reinforced material with protective sleeves — reduces impact from debris and dust |
| Interfaces | Standardised mounting interfaces on the frame side: pump station carriage, cable reel carriage, hydraulic line rack |
| Maintenance | Removable bottom coal plate for cleaning rails and frame of accumulated coal |
| Efficiency | Coordination of development and transport work improved by more than 30% |
| Testing | Functional testing and factory commissioning; every unit checked before shipment |
Specifications are as stated by the manufacturer at the time of publication and do not constitute a public offer. Our engineer confirms the exact figures for your configuration after receiving the project data.
Send us the conveyor parameters and the installation conditions — our engineer will prepare specifications and a quotation.
Request Technical Solution